Briefly:
• Consistent quality control in laser welding depends on pre-weld process validation, in-process monitoring, and post-weld inspection using both visual and non-destructive methods.
• U.S. operations must align with OSHA, ANSI, and ISO standards to remain compliant and produce structurally sound welds.
• Sectors such as aerospace, medical devices, and oil and gas demand the tightest tolerances.
Effective quality control separates reliable laser welding operations from those that produce costly rework or field failures. Across U.S. manufacturing, the stakes are especially high in precision-critical industries where a single defective weld can compromise an entire assembly.
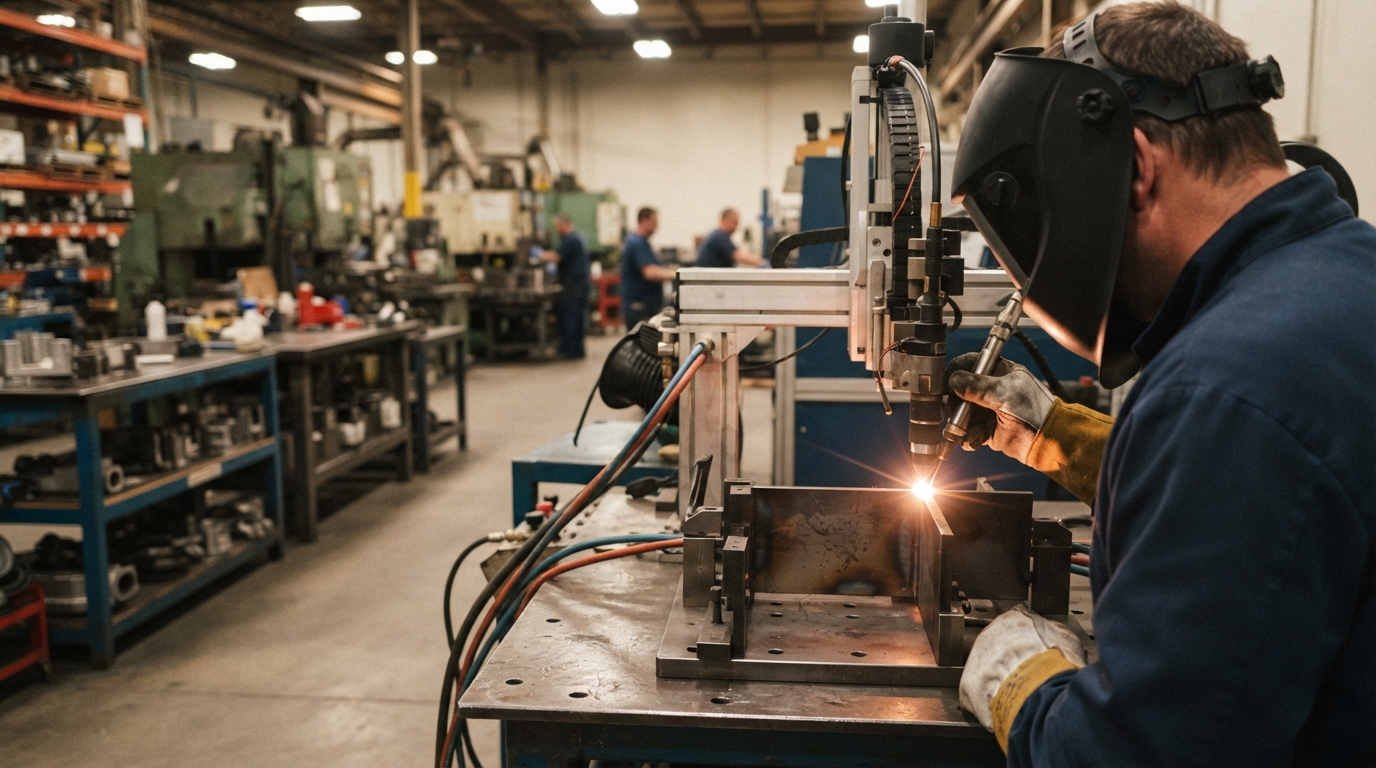
Industrial laser welding combines a concentrated beam of light with precise heat input to fuse materials with minimal distortion. Known for high speed, minimal distortion, and strong, clean joints, laser welding is gaining popularity in advanced manufacturing sectors like aerospace, automotive, and medical device fabrication. That precision advantage, however, only holds when a structured quality control framework is in place from start to finish.
Standards That Govern Laser Weld Quality in the U.S.
U.S. laser welding operations sit at the intersection of multiple regulatory and standards bodies. In the U.S., laser standards exist regarding the general safe use of lasers and the safe use of lasers in manufacturing environments, including ANSI Z136.1 and ANSI Z136.9. On the process quality side, laser welding must also meet welding quality standards such as ISO 15614-11, ISO 14732, ISO 13919 for defect criteria, and EN ISO 3834 for overall weld quality control.
ISO 15609-4 is an international standard that formulates laser welding’s Welding Procedure Standards (WPS), presenting a uniform welding approach for coherent and effective communication among manufacturers, inspectors, and regulators. Alongside it, ISO 13919 complements ISO 15609-4 and highlights certain conditions for optimal weld quality and tolerance, which manufacturers use to achieve optimal structural integrity, desirable joint geometry, and project-appropriate beam power.
For personnel compliance, OSHA’s nonionizing radiation standard (29 CFR 1926.54) requires that only qualified, trained personnel operate lasers. Facilities operating Class 3B or Class 4 lasers must also, according to the American Welding Society, appoint a qualified Laser Safety Officer (LSO) and maintain a documented Laser Safety Program.
The Three Pillars of Laser Weld Inspection
Weld inspection of laser and electron beam welded parts generally follows three distinct paths: visual inspection, destructive testing, and non-destructive testing (NDT). Each layer serves a different function and catches different defect types.
Visual Inspection Visual inspection involves looking at a weld with the naked eye and/or with some level of magnification, with inspectors typically checking for cracks, pits, surface pores, undercut, underfill, missed joints, and other aspects of the weld. It is the fastest and most cost-effective first pass.
Non-Destructive Testing (NDT) NDT methods allow inspectors to evaluate internal weld integrity without damaging the part. Connected sensors can monitor weld conditions during fabrication, providing real-time alerts for deviations, which minimizes rework and enhances traceability.
Destructive Testing Destructive testing is typically controlled by AWS D17.1, AWS 2680, and AWS 2681. These tests confirm mechanical properties such as tensile strength and ductility on sample coupons pulled from production runs.
Comparing Inspection Methods by Application
|
Inspection Method |
Best For |
Detects |
|
Visual / Magnification |
Surface defects, all sectors |
Cracks, pits, undercut |
|
Radiographic (X-ray) |
Aerospace, medical devices |
Internal porosity, voids |
|
Dye Penetrant (PT) |
Mold repair, gun components |
Surface-breaking cracks |
|
Laser Vision Scanning |
High-volume production |
Geometry, bead profile |
The rapid evolution of welding technology demands an equal progression of quality control, measurement accuracy, and digital data output that can only be captured and realized by laser technology. Laser scanning in particular has become a preferred tool for validating weld geometry against tight dimensional tolerances.
Pre-Weld and In-Process Controls That Prevent Defects
Reactive inspection catches problems after the fact. Proactive controls prevent them. Key pre-weld steps include:
• Material verification: Confirm base metal chemistry and cleanliness before welding begins.
• WPS documentation: A written Welding Procedure Specification defines laser parameters, travel speed, focal position, and shielding gas requirements.
• Fixturing and fit-up: Poor joint fit-up is a leading cause of porosity and incomplete fusion in laser welds.
In-process controls matter equally. On large-scale production lines, on-site uncertainties such as material inhomogeneity, residual impurities, and parameter fluctuations increase welding instability and can easily lead to welding defects. Real-time power monitoring and closed-loop feedback systems are now standard practice in high-output laser welding cells to catch parameter drift before it produces a defective part.
Reliable laser welding services for precision machined components depend on this layered approach. Micro Weld, Inc serves industries including aerospace, medical devices, mold repair, oil and gas, and gun components across the USA, applying precision laser and TIG welding processes to parts where quality failures are not an option.
Frequently Asked Questions
What is the most common defect in laser welding? Porosity and incomplete fusion are among the most frequently cited defects, often caused by contamination, poor fit-up, or parameter drift during the weld cycle.
Which ISO standard applies to laser weld defect acceptance criteria? ISO 13919 establishes defect acceptance levels for laser and electron beam welds, covering criteria for steel, nickel, titanium, and aluminum assemblies.
Does OSHA regulate laser welding operations directly? Yes. OSHA’s 29 CFR 1926.54 standard requires qualified personnel to operate lasers, and the General Duty Clause obligates employers to identify and control hazards even where specific guidance is limited.
How does ISO 13485 certification affect laser welding quality control? ISO 13485 is a quality management system standard specific to medical devices. Shops certified to this standard must document and control every step of the welding process to ensure traceability and repeatability for medical applications.
Quality control in laser welding is not a single checkpoint at the end of a job. It is a system built from verified standards, trained personnel, documented procedures, and layered inspection methods applied before, during, and after every weld. Operations that treat these controls as foundational rather than optional consistently produce parts that meet the tightest tolerances demanded by U.S. aerospace, medical, and industrial customers.